Teanga
Faigh luachan
Faigh luachan
 Áit / Fearas / Meaisín Táthú Butt na Náisiún Aontaithe / Meaisín Táthú Butt Oibrithe Lámh UN1 / UN1-150KW Cruach-Bharra Cruach Meaisín Táthú Butting
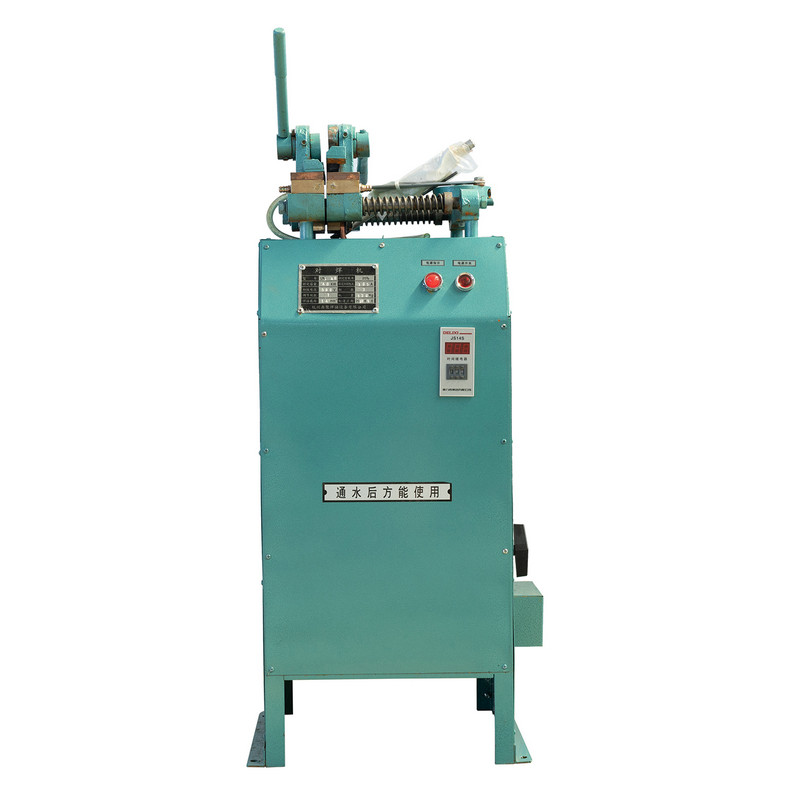


Tá dearadh cuimsitheach ag an meaisín táthúcháin barra cruach UN1-150kW, a chuimsíonn claochladán táthúcháin, leictreoid stáiseanóireachta, clamp leictreoid inchoigeartaithe, innealra brú-chothaithe, agus córais rialaithe. Ar fud na dtionscal éagsúil, tá sé thar a bheith tábhachtach go dtáirgeann sé táthaithe ardchaighdeánacha ar ábhair amhail cruach ísealcharbóin agus miotail neamhfheiriúla, lena n-áirítear copar, alúmanam, agus a gcóimhiotail. Cinntítear cobhsaíocht agus iontaofacht i bhfeidhmíocht táthú trí úsáid a bhaint as conraitheoir AC sa phríomhchiorcad lasctha. Ina theannta sin, déantar an meaisín a innealtóireacht ar mhaithe le cothabháil a dhéanamh.

Sonraíochtaí
|
Múnla |
Aonad |
UThuaidh1-1KW |
UN1-3KW |
UN1-10KW |
UN1-16KW |
UN1-25KW |
UN1-40KW |
|
|
Príomhvoltas |
V |
220 |
220 |
380 |
380 |
380 |
380 |
|
|
Cumas rátáilte |
KVA |
1 |
3 |
10 |
16 |
25 |
40 |
|
|
Sruth príomhúil rátáilte |
A |
4.5 |
13.6 |
26 |
42 |
66 |
105 |
|
|
Ré ualaigh rátáilte |
% |
8 |
15 |
20 |
20 |
20 |
20 |
|
|
Gan aon voltas ualaigh |
V |
0.65-2.0 |
1.55-3.0 |
1.65-2.4 |
1.98-3.01 |
2.25-3.58 |
3.1-5.2 |
|
|
Céim Rialála Voltais Tánaisteach |
céimeanna |
8 |
8 |
7 |
7 |
7 |
7 |
|
|
Fórsa trína chéile uasta |
N |
10 |
180 |
500 |
1000 |
1000 |
1000 |
|
|
Stróc beathú uasta |
mm |
3 |
5 |
22 |
22 |
22 |
22 |
|
|
Achar uasta an fhód |
mm |
7 |
10 |
10 |
16 |
16 |
16 |
|
|
Trastomhas táthú uasta |
Cruach ísealcharbóin |
mm |
0.6-2.0 |
1.0-5.0 |
3.0-8.0 |
3.5-10.0 |
5.0-12.0 |
6.0-14.0 |
|
Copar |
mm |
0.6-1.6 |
1.0-2.5 |
2.5-5.0 |
3.0-6.0 |
4.0-8.0 |
6.0-10.0 |
|
|
Alúmanam |
mm |
0.6-1.6 |
1.0-3.0 |
2.5-5.0 |
3.0-6.0 |
4.0-8.0 |
6.0-12.0 $ $ $ |
|
Táirgí Molta
COINNIGH I dTEAGMHÁIL
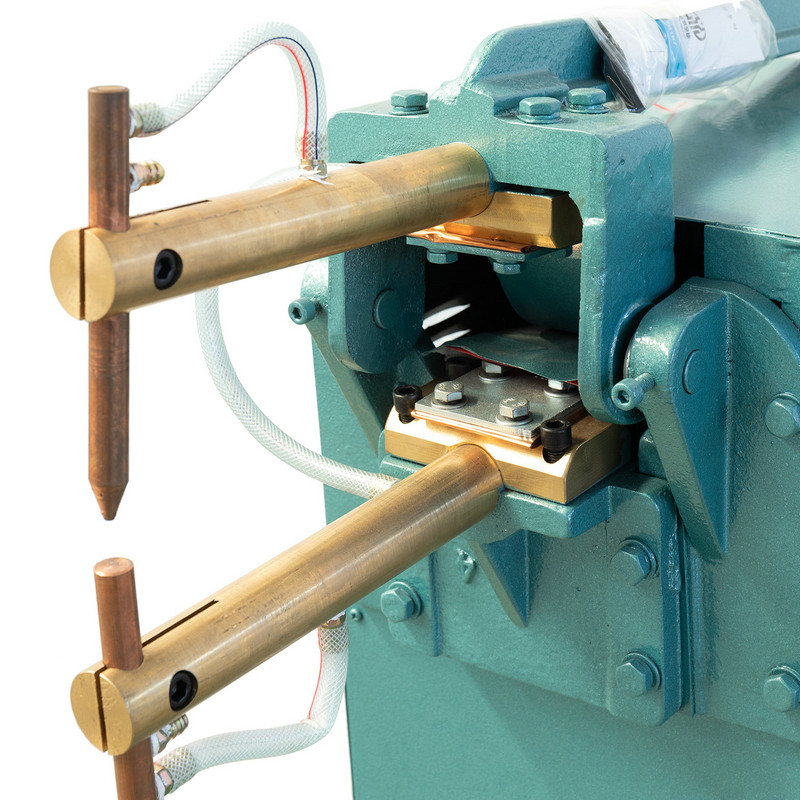
Every weld is a production decision. When you choose an electrical welding machine, you are really choosing how to balance weld quality, cycle time, and operator effort on your floor. After buil...
LÉIGH TUILLEADH
Understanding Resistance Butt Welding and the Role of Flash Weld Technology Joining two metal bar ends face to face without filler material is one of the oldest challenges in metal fabrica...
LÉIGH TUILLEADH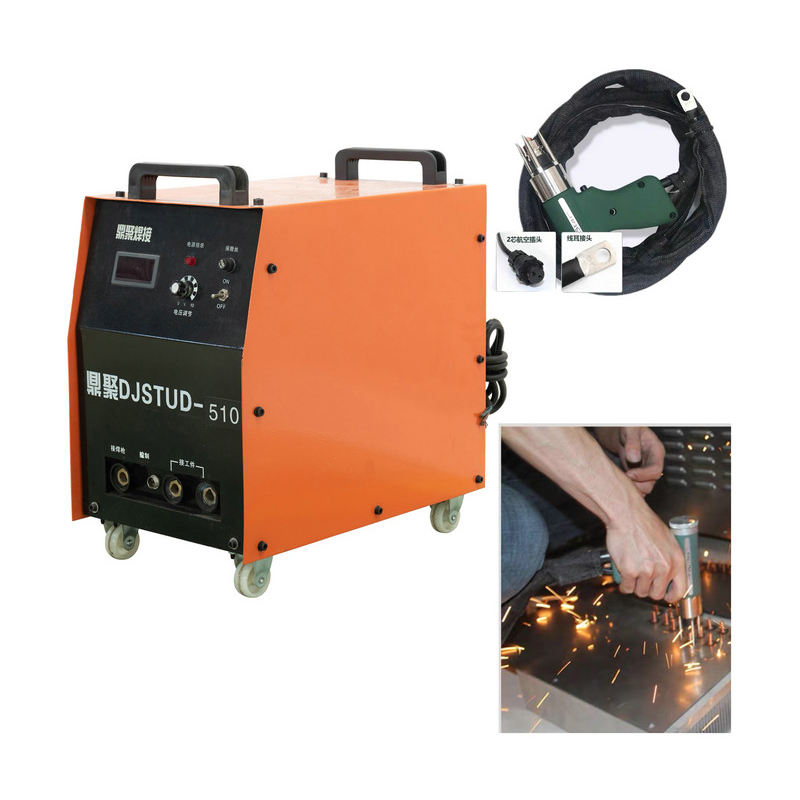
Understanding Stud Spot Welding Technology Today Fastening components to metal panels without drilling or riveting has become a standard requirement across sheet metal fabrication, shipbui...
LÉIGH TUILLEADH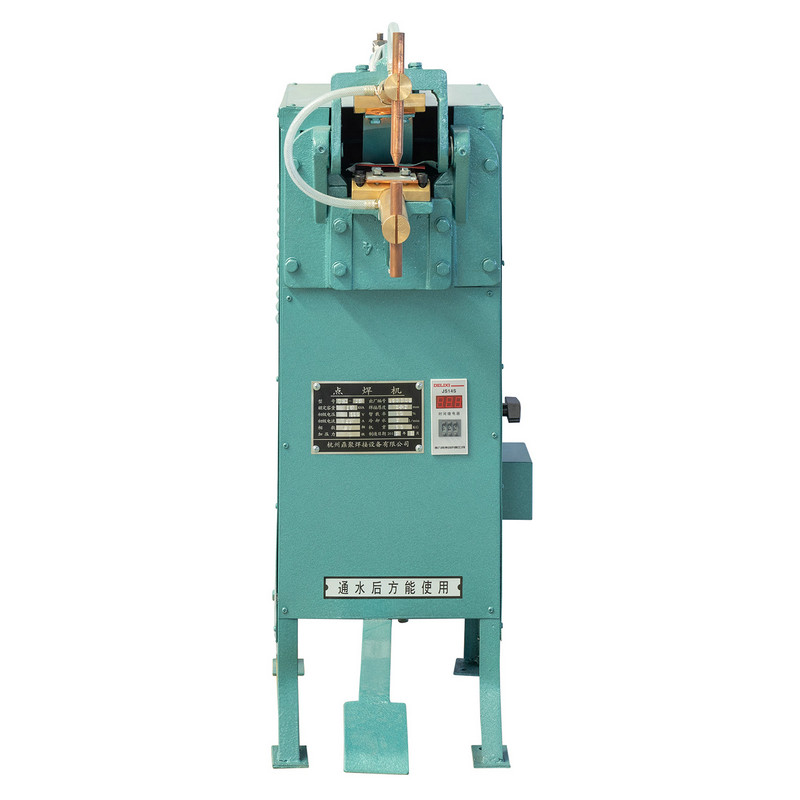
Spot Welding Machine Categories and How They Differ Resistance spot welding equipment is generally divided by how the electrode force is generated and applied. Mechanical foot-pedal units ...
LÉIGH TUILLEADH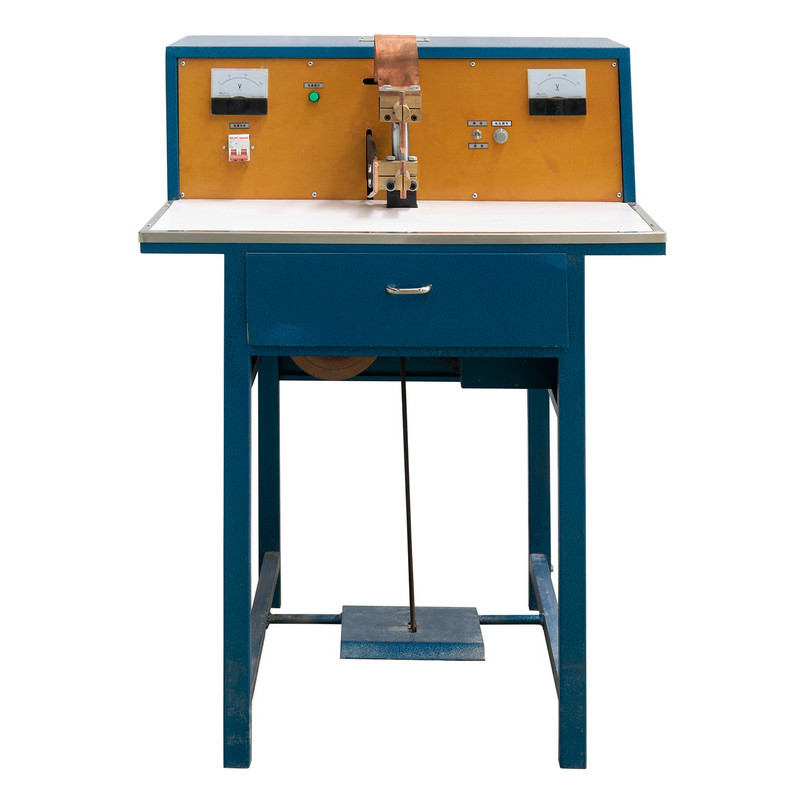
Why Heat Is the Hidden Bottleneck in Spot Welding Is imeacht rialaithe teirmeach é gach spot-táthú frithsheasmhachta, ina chroílár. Téann cuisle gairid, dian srutha trí dhá leathán miotail...
LÉIGH TUILLEADH
Why Electrode and Controller Maintenance Determines Weld Quality In resistance spot welding, the quality of every joint depends on two components working in sync: the electrode that delive...
LÉIGH TUILLEADH
Táirge
Cód QR